This guide explains how to evaluate and source item 19655 with a focus on supplier reliability, specification alignment, and procurement readiness. Objectively, the keywords relate to procurement identifiers, sourcing workflows, and due-diligence criteria that help organizations reduce lead-time risk, verification errors, and mismatched specifications across supply chains.
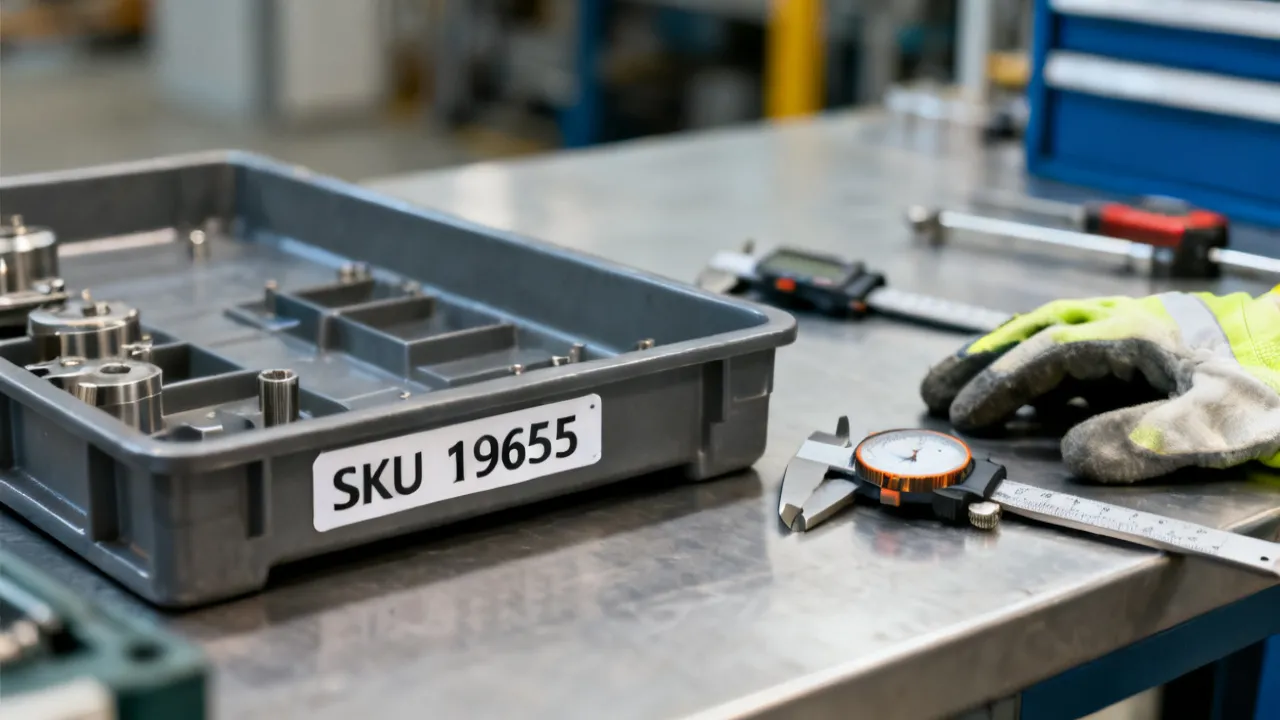
When sourcing item 19655, the very important step is ensuring the product you receive matches the intended specification—down to part numbers, tolerances, packaging requirements, and documentation. In practice, “supplier fit” matters as much as the item identifier itself: a precise match reduces rework, prevents assembly downtime, and supports smoother incoming inspection.
This article integrates the provided keywords (shown as placeholders in your brief) by treating them as procurement variables—such as internal reference identifiers, catalog terms, and sourcing descriptors—then translating them into a dependable evaluation approach around 19655. Instead of relying on assumptions, you’ll use a structured checklist to confirm compatibility, validate supplier capability, and minimize operational surprises.
Throughout the guidance below, the consistent theme is evidence over inference. In procurement, “close enough” is rarely close enough: even small configuration differences can create downstream problems such as incorrect fit in assemblies, compliance gaps, or failure to meet testing and traceability requirements.
An identifier such as 19655 often functions as a stable reference for procurement teams. However, identifiers alone do not guarantee quality or compatibility—especially when similar items exist across revisions, suppliers, or regional manufacturing lots. For that reason, experienced procurement and supply-chain professionals treat an ID as a starting point for verification rather than a complete description.
In objective terms, item references are commonly tied to one or more of the following:
Therefore, when the keyword set includes terms that represent “catalog-like” or “spec-like” descriptors, the operational goal is consistent: align what the supplier offers with what your engineering and operations teams require.
To make this practical, procurement teams typically use the item identifier to retrieve a “spec packet” internally. That spec packet often includes drawings, tolerance stack assumptions, required test standards, and any regulatory or customer-specific obligations. If a spec packet is incomplete or not version-controlled, item IDs like 19655 become less meaningful—because you lose the canonical target that makes verification possible.
In mature organizations, the identifier also helps with auditability: if a question arises later (“Why did we buy this?” “Which revision did we receive?” “Which test data was used?”), the procurement record should connect the delivered lot back to the contract documents and acceptance evidence. That is why correct item reference mapping is foundational.
From an industry expert’s perspective, supplier sourcing for an item like 19655 typically fails for predictable reasons: unclear specifications, undocumented changes, inadequate traceability, or inconsistent packaging that affects receiving inspection outcomes. The solution is a methodical evaluation that covers capability, quality assurance, and procurement readiness.
Key areas to verify include:
Request and compare the supplier’s item documentation against your internal requirements. Ensure you confirm:
If the keywords in your brief indicate alternate catalog terms or internal codes (the placeholder strings), treat them as aliases that must be resolved to one canonical specification for 19655.
In real purchasing practice, specification alignment is where many issues originate. Common failure patterns include:
To prevent these, procurement teams often formalize a “spec confirmation” step before issuing a purchase order. This is not just an engineering task—procurement is accountable for ensuring the purchase order and contract attachments match the intended configuration and evidence expectations.
Even when a part looks correct, documentation quality determines how smoothly production proceeds. Evaluate whether the supplier provides:
Where appropriate, validate quality systems using objective standards such as ISO 9001. For general context on ISO 9001, see the ISO overview and requirements documentation available through ISO’s official materials (ISO does not publish “pass/fail” ratings, but the standard itself provides a widely recognized baseline).
For item 19655, it is helpful to think beyond “do they have a certificate.” The question is whether their quality system enables predictable delivery of evidence at the level required by your receiving department and your internal audit expectations.
Examples of what “quality readiness” can mean for incoming inspection include:
In regulated industries (medical, aerospace, defense, certain energy applications), suppliers may also need to follow additional quality or compliance frameworks. Even if not regulated, customers increasingly expect traceability and documented process controls.
Lead times are frequently quoted optimistically, then adjusted after scheduling constraints. A professional approach is to ask for:
When you evaluate “supplier details” (as referenced in your brief) the objective is not to chase lowest cost at any price. Instead, balance procurement cost with delivery reliability and downstream risk reduction.
For item 19655, “delivery reliability” is not only about the promised ship date. It is also about:
Procurement teams often incorporate lead-time reliability into sourcing decisions by comparing supplier performance history, or by negotiating contractual terms that define what happens when lead times slip.
Your brief mentions price information, but no numeric price or currency value was supplied. In professional procurement, pricing for an item like 19655 typically varies based on factors such as:
To keep the analysis objective, it’s top to structure the quote comparison around total landed cost components rather than unit price alone. Total landed cost usually includes freight, handling, duties/taxes (where relevant), and the cost of inspection/receiving labor.
When you request quotes, ask suppliers to break down price elements so you can compare like-for-like. This is especially important if the keywords in your brief indicate multiple sourcing descriptors that may correspond to different compliance packages or product revisions for 19655.
Below are common pricing components that procurement teams often miss when they compare unit rates only:
A disciplined approach uses a “cost of quality” lens: if a supplier is cheaper but your receiving team will spend extra time verifying or reworking, or if the part is more likely to fail acceptance testing, the true cost is higher.
Even after you select a supplier, the real risk management continues during receiving. A robust incoming verification workflow typically includes:
This approach reduces the likelihood that the “wrong-but-close” version of 19655 enters production—an issue that can be costly to fix after assembly.
To expand on this workflow, it is useful to define each step’s objective and typical outputs.
The aim is to ensure paperwork and physical items correspond. In practice, receiving teams verify:
If there is a mismatch, a well-defined receiving hold prevents “silent failures”—where a wrong revision or unapproved configuration enters stock.
Visual inspection should not be treated as the only gate. Instead, it is a first-line check for obvious discrepancies like:
Visual inspection also helps triage whether dimensional sampling needs to be expanded.
What you measure depends on the canonical spec for 19655. In general terms, receiving sampling may include:
The key is that sampling should be designed around acceptance criteria—not convenience. For example, if the spec includes tolerances that drive assembly performance, those tolerances should be prioritized in receiving inspection.
Traceability isn’t just for regulatory environments. It is crucial whenever you need to perform root-cause analysis for field failures, warranty claims, or quality escapes.
Receiving teams should record traceability identifiers so that later, if a problem is discovered, you can identify:
This step must align with how your ERP/MES systems track lots. Otherwise, traceability effort becomes wasted effort because it cannot be used downstream.
Disposition options should be clear: accept, hold for review, or reject. A disciplined process includes:
When disposition is recorded properly, it also improves supplier performance over time by providing measurable feedback.
Your brief does not specify a city or country, and the keywords also do not explicitly embed one. Still, in localized procurement practice, communication style matters. For example, in many regions, buyers expect concise technical confirmation in addition to commercial terms. Common professional habits include:
If your internal procurement team uses standardized templates, align your supplier communications to those templates so that 19655 is consistently handled through quoting, ordering, and receiving.
Communication is not only about language; it is also about format consistency. Many procurement failures are “process failures” where the supplier receives an incomplete package or misinterprets which document is authoritative. To minimize this risk, best practice is to:
If your internal workflow includes placeholder keywords that correspond to supplier-provided terms, ensure that the supplier confirms those terms in writing and links them to the canonical specification for 19655.
The table below summarizes common approaches for sourcing item 19655. It is written as a supplement to the main workflow, focusing on conditions and requirements rather than promotional claims.
| Sourcing approach | Typical fit | Key conditions/requirements | Verification evidence to request |
|---|---|---|---|
| Direct supplier purchase | When specification control is critical | Exact part number mapping to 19655, revision confirmation, documentation completeness | CoC/test reports, lot traceability, packaging spec, drawing |
| Authorized distributor route | When you need faster procurement scheduling | Distributor must provide supplier documentation and warranty/support terms | Original manufacturer documentation, traceability references |
| Multi-sourcing procurement (two+ suppliers) | When continuity and resilience are priorities | Comparable quality criteria across sources; standardized acceptance testing | Cross-supplier spec comparison, sampling test results, consistent labeling |
| Custom/bespoke configuration | When 19655 is part of an assembly or modified specification | Written engineering change record; documented compliance scope | Updated drawings, change history, acceptance criteria |
While the table is simple, it encodes an important procurement principle: the “fit” of a sourcing path depends on how strict your specification control must be and how quickly you need product availability.
For example, direct supplier purchase often supports strongest traceability and documentation alignment. Distributor routes can improve scheduling but may introduce additional steps in documentation verification. Multi-sourcing provides resilience but can complicate consistency if suppliers interpret requirements differently. Bespoke configurations require controlled engineering change processes to ensure documentation and acceptance criteria remain aligned with the intended functional performance.
Use the steps below as a practical, objective sequence. Adjust the depth based on your industry requirements (e.g., regulatory, safety-critical, or high-precision use cases).
This sequence works particularly well because it front-loads clarity. Instead of trying to fix mismatches after shipment, it establishes the required evidence and acceptance method before manufacturing and shipping decisions are finalized.
Procurement due diligence also improves negotiation outcomes. When you can point to specific documentation requirements (and show that you have a consistent internal acceptance framework), suppliers are less able to argue ambiguity later. That strengthens both your operational control and contractual posture.
Even without location-specific constraints, many buyers apply conditions that help keep sourcing objective and auditable. Typical requirements for an item like 19655 include:
Procurement teams often formalize these requirements in purchase order terms and in attached technical documents. A common maturity step is to include:
When requirements are ambiguous, disputes increase. When requirements are evidence-driven and traceable, suppliers understand what they must deliver and receiving teams can verify systematically.
To avoid unverified or exaggerated claims, this guide relies on widely accepted procurement and quality concepts. For authoritative background on quality management systems, consult:
These references support the process logic described above—especially the emphasis on documentation, traceability, and verification—without asserting specific performance numbers for individual suppliers or markets.
It can be useful to connect this to procurement practice in a direct way:
Even if you are not explicitly performing “standards compliance audits,” these frameworks provide a logic for how to structure requirements and verification steps.
While the receiving verification workflow provides the core steps, procurement and quality teams often benefit from additional detail—especially when multiple internal departments are involved (warehouse, QA, engineering, and procurement).
The following expanded checklist is designed to be practical. It assumes that 19655 is a part where specification alignment, documentation, and traceability are critical. You can adapt the sampling approach to your risk profile.
Receiving verification starts earlier than most people think. Prior to arrival, you can reduce risk by:
This step prevents the “administrative delay” situation where the shipment sits waiting for information, increasing the chance that items are stored without proper quarantine labeling.
Upon arrival, items should be treated as unverified until documentation and sampling are completed. A best practice is to:
Because packaging can affect finish, labeling can affect traceability, and damage can affect fit or corrosion resistance, the quarantine stage is a quality control mechanism—not just an administrative step.
Document match should include more than verifying “19655 appears somewhere.” A robust document match verifies:
If your internal procedures require a specific template (for example, “CoC must list standards X and Y”), ensure that the supplier’s document matches your template requirements or your system can ingest their data format.
Visual inspection should be aligned with what receiving can observe quickly without special equipment. For 19655, visual inspection may include:
If a spec requires that a certain finish thickness be maintained, visual inspection alone is insufficient. However, visual inspection can identify conditions that make dimensional verification more likely to fail.
Sampling should be based on risk and spec-critical features. For item 19655, define:
In many procurement programs, the sampling strategy changes depending on history. If the supplier has delivered 19655 reliably for a long period, sampling might follow a reduced rate. If there is a new supplier, new revision, or previous nonconformance, sampling should increase.
Some items are best verified via functional checks rather than only dimensional checks. If 19655 is part of a system where performance matters, functional verification may include:
Functional tests require careful planning because they can be time-consuming and may not always be feasible for high-volume receipts. That is why suppliers often provide documentation and test evidence to reduce the need for full in-house functional testing.
Traceability capture should map external identifiers to internal records. For each lot of 19655, store:
When traceability capture is incomplete, quality teams cannot perform effective root-cause analysis. This can create costly delays during investigations and can reduce trust in supplier evidence.
If nonconformance occurs, disposition needs documented evidence. Nonconformance evidence should include:
Then procurement coordinates corrective action with the supplier. Corrective action should not only address the defective unit but also the process root cause that allowed nonconformance to occur.
Unit price comparisons can be misleading. For 19655, what you really compare is the “delivered cost” plus the “cost of verification and risk.” A disciplined cost model helps you make consistent decisions across different supplier offers.
Below are practical ways to build that model.
Total landed cost commonly includes:
Even if your procurement team does not fully calculate all elements, you should at least acknowledge them when comparing quotes. In some cases, the supplier with the slightly higher unit cost may deliver lower total cost due to faster lead times (reducing expedite costs) or more complete documentation (reducing QA time).
Consider:
If your organization tracks cost-of-nonquality (CONQ), incorporate those data into the procurement decision. If you do not currently track it, start by estimating the costs of common receiving issues such as:
These costs are often far larger than unit price differences.
Procurement decisions should also include contractual terms. For example:
If a supplier offers lower price but requires you to accept higher documentation risk or weaker replacement terms, the true total cost can become higher.
Many procurement teams evaluate suppliers on whether they meet minimum requirements. For a critical item like 19655, it is more useful to evaluate whether the supplier consistently meets requirements under real production conditions.
Capability and capacity can be assessed through a combination of documentation review and practical signals.
Capability often shows up in:
Even if you do not audit their full quality system, you can ask targeted questions and review evidence. For example, you can request samples of past CoC/test packages for similar parts and verify whether documentation includes the right identifiers and references.
Capacity shows up in whether the supplier can handle your order volume and schedule without cutting corners. Consistency shows up in whether successive deliveries follow the same documentation and labeling patterns.
Procurement can probe this by requesting:
When evaluating multiple sourcing options, consistency is particularly important. If Supplier A ships correctly documented lots but Supplier B has labeling variations, you may reduce risk by standardizing your receiving reconciliation process—yet you may still increase receiving time.
For items like 19655, revision control is a major risk lever. A disciplined procurement program recognizes that “same part number” can still mean different realities if revision levels change.
To manage revision risk, you can implement a first-article approval workflow and ensure that:
First-article approval is especially important when:
Implementing first-article control reduces the chance that a large batch fails inspection later. Even if it adds short-term time, it often saves significant time and cost overall.
Even with disciplined sourcing, nonconformance can occur. What matters is how quickly and effectively the organization responds, and whether supplier corrective action addresses root causes.
A typical nonconformance playbook for 19655 includes:
Immediately quarantine nonconforming units and associated lots. Prevent issuance to production. Record lot identifiers and quantities impacted.
Collect evidence such as photos, measurement records, and document discrepancies. Ensure evidence is consistent and traceable back to specific lots and inspection steps.
Notify the supplier with:
Require a corrective action response that includes:
After corrective action, perform receiving checks for subsequent lots. Depending on the criticality of the nonconformance, you may require additional sampling or pre-shipment inspection evidence.
This playbook ensures learning and reduces recurring failures, which is crucial for long-term supply continuity.
Multi-sourcing can strengthen supply continuity, especially for items with long lead times or supplier-specific constraints. However, multi-sourcing introduces variability risk if suppliers interpret specifications differently.
To multi-source 19655 successfully, you need:
When multi-sourcing is done correctly, you achieve resilience without losing control. When it is done informally, you may end up with more nonconformances due to inconsistent documentation and labeling patterns.
One practical approach is to maintain a “supplier equivalence dossier” for 19655 that includes:
This dossier acts as a centralized control mechanism across procurement, QA, and engineering teams.
Your brief indicates that the provided keywords should be integrated into the procurement approach as variables. In practice, these placeholder keywords typically represent something like:
The procurement discipline required here is mapping. Every keyword variable must be mapped to the canonical spec for 19655.
To implement mapping, you can maintain a crosswalk table internally. For example:
Then, when suppliers provide quotes or documentation, you validate that their provided terms correspond to the mapped canonical specification. This prevents a common failure: the supplier believes they are quoting the right item because the term looks similar, but your internal canonical specification differs in a critical way (finish, tolerance, or compliance scope).
It usually functions as a catalog or internal reference identifier. In practice, 19655 should be treated as a key to retrieve the correct specification and revision—not as proof of compatibility by itself.
Procurement should always connect the item identifier to the authoritative drawings, engineering acceptance criteria, and documentation expectations that define what “correct” means.
Request the supplier’s part documentation (drawings, revision level, and any change history) and compare it to your internal acceptance criteria. Require written confirmation that the delivered item matches the specified revision scope of 19655.
If your organization uses document control, ensure the supplier’s documentation references your authoritative revision. If the supplier provides a “newer” revision, confirm it has been approved through your engineering change process before accepting it.
No. For item 19655, evaluate total landed cost and risk factors: documentation completeness, lead-time reliability, receiving inspection effort, and replacement/nonconformance policy.
A supplier might offer a lower unit price but require additional receiving work, or might have a track record of documentation incompleteness that increases hold time and impacts production readiness.
At minimum, a packing list that references 19655 and traceability/quality documentation relevant to your application is standard practice. Typical examples include a CoC and test reports when required.
The more critical the application, the more you should define the documentation scope in advance so receiving can verify quickly and consistently.
Use a documented nonconformance process: quarantine the lot, record evidence from receiving inspection, notify the supplier with photos/measurements, and request corrective action aligned to agreed contractual terms for replacement or refund.
Ensure that nonconformance evidence includes lot identifiers and references to acceptance criteria. This helps suppliers respond effectively and helps your organization defend acceptance decisions during audits.
Multi-sourcing can increase resilience, but only if acceptance criteria and verification methods are standardized across suppliers. For 19655, it’s very useful when supply continuity and risk reduction are strategic priorities.
If you multi-source, create supplier-specific verification profiles that align with the canonical spec and receiving procedures. This avoids inconsistent inspection and helps maintain comparable evidence across suppliers.
Do not rely on wording alone. Map both descriptions to the canonical specification for 19655 using drawings, dimensional requirements, material grades, and compliance scope. Request clarification and written confirmation.
Then verify at receiving that the supplier’s physical shipment and documents match your canonical spec. Wording differences are often harmless, but they can also signal a configuration mismatch that only becomes visible through dimensional checks or documentation verification.
Sourcing 19655 successfully comes down to disciplined verification—spec alignment, quality documentation, realistic lead-time planning, and an incoming inspection workflow that catches mismatches early. By approaching supplier evaluation as an evidence-driven process and treating pricing as part of total procurement readiness (not just a unit rate), organizations can reduce downtime risk and improve consistency across orders.
If you share additional specifics—such as the industry use case, required documentation, target quantity, and the exact meaning of the placeholder keywords in your internal system—I can refine the checklist and provide a tighter acceptance/verification matrix for 19655.
Striking the Perfect Balance: Navigating Premiums and Out-of-Pocket Expenses in Senior Insurance Plans
Explore the Tranquil Bliss of Idyllic Rural Retreats
How to Make Lasting Memories at Disneyland Attractions
4rkojvsx Technology: Industry Insights and Buying Guide
Affordable Phones and Plans for Seniors
Affordable Full Mouth Dental Implants Near You
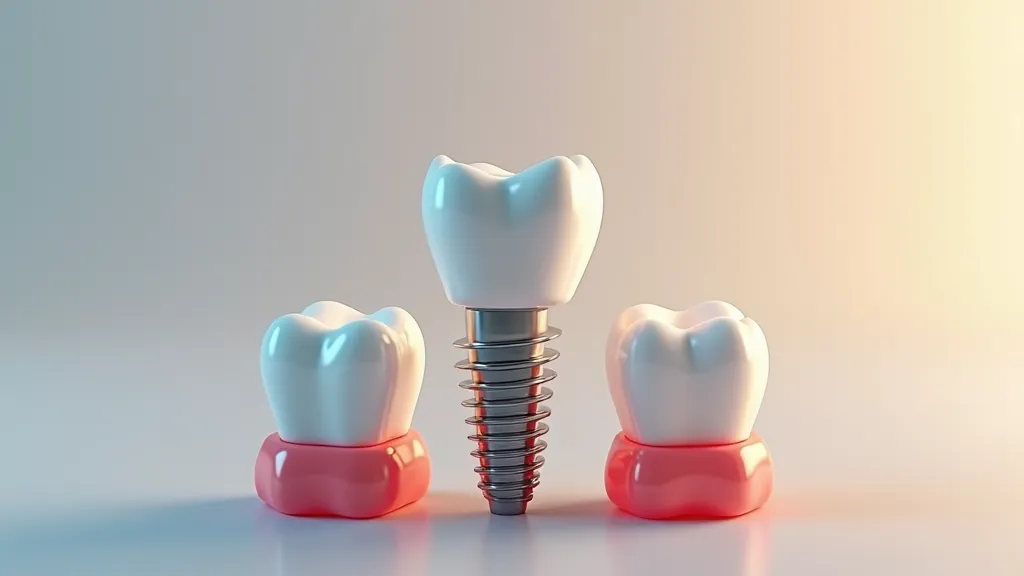
Unlock the Top Kept Secrets to Finding Your Ideal Dentist for Flawless Dental Implant Results!
Discovering Springdale Estates
Unveiling RS Sul Telecom Services
Smart Strategies to Slash Costs on Your Roof Replacement Endeavor
Opening Remarks: Smart budgeting doesn't mean cutting corners on quality. This guide will delve into cost-effective approaches for roof replacement that maintain high standards.
Unlocking the Secrets of Preschool: Your Ultimate Guide to Early Childhood Education Programs
The significance of early childhood education programs is paramount in shaping the foundational stages of a young child's life. These educational experiences aim to furnish children with a diverse skill set before they face the structured environment of elementary education. Such programs offer a dynamic and engaging atmosphere where children's natural curiosity leads to the broadening of their thought processes. Moreover, they focus on rectifying behavioral patterns and fostering positive principles and routines.
Enhance Your Smile: Essential Gum Care Tips After Teeth Replacement
After getting new dental implants, it's crucial to look after your gums to aid recovery, shield against infection, and enhance the durability and function of the implants. This discussion delves into the key methods and top tips for gum care that are vital to keep your gums robust and healthy after your procedure.
Unlock the Secrets to Championing Fair Pay: A Guide to Fighting for Competitive Nurse Salaries at Your Hospital
To effectively navigate the intricacies of nurse compensation in healthcare institutions, a thorough understanding goes beyond the basics. Strategic advocacy is essential, honoring nursing as a critical profession while also deeply comprehending the economic aspects of healthcare. This article lays out systematic methods to advocate for fair remuneration for nurses, aimed at closing the divide between managerial policies and the realities nurses face daily.
Protect Your Golden Nest Egg: Smart Strategies and Essential Precautions for Securing Your Gold Investments
Investing in gold requires more than just purchase; diligent protection and a strategic mindset are crucial. A secure gold investment is built on thoughtful planning, alert risk management, and the capacity to adapt to changes. We'll explore various ways to protect these investments from the diverse challenges they face.
Unlock Higher Earnings: Master the Art of Leveraging Your Nursing Expertise for a Hefty Pay Raise!
Unraveling the complexity of the payment landscape in nursing isn't for the faint-hearted, yet it's a manageable task with a strategy in place, enhancing one’s prospects for improved salary through skill and knowledge. This delicate dance of upholding patient care while seeking just rewards is a path all nurses must walk. Grasping the elaborate character of the nursing role and what propels one's income forward is crucial. Within this paper, we dissect insightful methods to maximize the impact of your nursing qualifications.